
Description
Concave form cutter NFRk DIN 6518 — dimensions, material and tool specifications
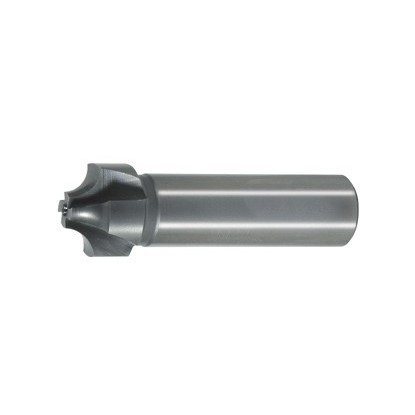
Concave corner rounding cutter R8 mm type NFRk made of high-speed steel (HSS) HSS (hardness 64 HRC) conforming to the standard DIN 6518. The cutting diameter Ø24 mm combined with 4 cutting edges ensures stable and efficient machining of large-radius quarter-round profiles. The Weldon shank Ø16 mm ensures rigid clamping under the substantial cutting forces encountered during form milling.
| TECHNICAL DATA | |
|---|---|
| Cutter type | Concave quarter-round 8 mm DIN 6518 |
| Radius R | 8 mm |
| Cutter diameter | Ø24 mm |
| Diameter D1 | 8 mm |
| Overall length L | 71 mm |
| Shank length I | 48 mm |
| Shank diameter d | Ø16 mm |
| Number of cutting edges Z | 4 |
| Material | HSS (high-speed steel) |
| Standard | DIN 6518 |
| Shank type | Weldon straight shank |
Workpiece materials and compatibility by ISO material group
The R8 mm HSS concave quarter-round radius cutter is designed to form large rounded edges on heavy industrial workpieces. The radius R8 mm is used on machine frame components, load-bearing structures, pump and turbine housings, and wherever edge rounding serves a structural function while also eliminating stress raisers. The large cutting diameter of Ø24 mm minimizes vibration during machining.
| Mat. group | Material | Vc [m/min] | fz [mm/tooth] | n [rpm] | F [mm/min] |
|---|---|---|---|---|---|
| P 1.1 | Structural steel ≤500 N/mm² | 28 | 0.067 | 371 | 99 |
| P 1.5 | Alloy steel 850–1000 N/mm² | 16 | 0.067 | 212 | 57 |
| M 2.1 | Austenitic stainless steel | 18 | 0.059 | 239 | 56 |
| M 2.3 | Martensitic stainless steel | 12 | 0.051 | 159 | 32 |
| K 3.1 | Gray cast iron | 22 | 0.085 | 292 | 100 |
| K 3.3 | Ductile cast iron | 28 | 0.085 | 371 | 127 |
| N 6.2 | Brass, bronze | 28 | 0.067 | 371 | 99 |
| N 7.1 | Aluminum — Al-Si alloys | 80 | 0.053 | 1061 | 226 |
| N 7.2 | Pure aluminum | 200 | 0.069 | 2653 | 735 |
| S 8.1 | Thermoplastics | 96 | 0.053 | 1273 | 271 |
For profile milling with a corner rounding cutter, use down milling (climb milling) for a better surface finish. For soft materials (Al, Cu), use higher cutting speeds and lower feed per tooth to avoid built-up edge (BUE).
hardness 64 HRC
profile R8 mm
clamping Ø16
standard DIN 6518
The R8 mm HSS cutter to DIN 6518 is suitable for machining structural steels (ISO groups 1.1–1.8), stainless steels (2.1–2.3), gray and ductile cast iron (3.1–3.5), copper alloys (6.1–6.4), aluminum and its alloys (7.1–7.4) and plastics (8.1–8.3). A cemented carbide cutter should be used for materials with a hardness above 45 HRC.
The concave radius cutter (NFRk) with a radius of R8 mm leaves a convex quarter-round edge on the workpiece. The R8 mm convex radius cutter (NFRx) cuts a concave profile in the material. Both types are standardized to DIN 6518 and are selected according to the required workpiece geometry.
For a cutter with a Ø16 mm Weldon shank, the optimal solution is a collet chuck ER32 (clamping range 2–20 mm) with an ER collet matching the shank diameter. ER collet chucks provide concentric clamping with radial runout below 0.01 mm, resulting in a better surface finish during profile milling. The ER collet distributes clamping force evenly around the entire shank circumference, eliminating the risk of tool deformation.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.