 Polski





- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
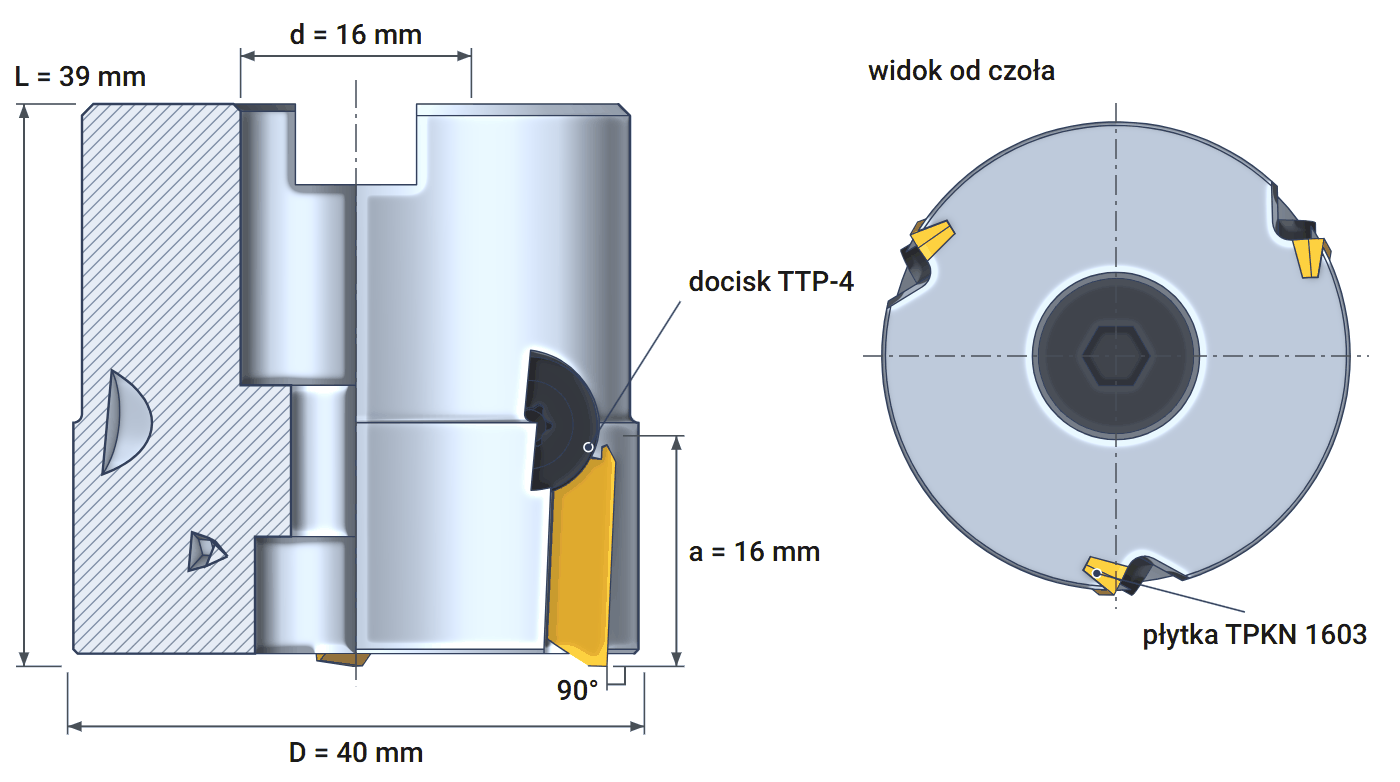
Ø40 mm milling head – for face milling with TPKN 1603 inserts
Technical data and dimensions – Varel 220.17, mounting bore 16 mm
| Technical data | |
|---|---|
| Head diameter D | 40 mm |
| Mounting bore d | 16 mm |
| Head height L | 39 mm |
| Cutting section height a | 16 mm |
| Max. depth of cut | 12 mm |
| Entering angle | 90 degrees |
| Number of inserts Z | 3 |
| Inserts | TPKN 1603, e.g., TPKN 1603 PDSR |
| Coolant supply | external |
| Head type | 220.17 |
| Manufacturer | Varel |
Diameter40 mm
Depth of cutup to 12 mm
Inserts3 × TPKN 1603
Coolant supplyexternal
Ø40 mm milling head Varel 220.17 cuts at a 90° angle with three TPKN 1603 inserts. This head is designed for face milling flat surfaces and milling square shoulders. It machines steel and stainless steel. It removes up to 12 mm of material in one pass. The insert has three edges: when one becomes dull, index the insert and continue machining.
This is a type 220.17 milling head for metal with replaceable inserts. Instead of a shank, it has a 16 mm bore with a transverse slot. It mounts on a milling arbor, and the arbor drive keys transmit torque. The inserts have no hole – each is held in its pocket by a clamp with a screw. The body has no coolant channels, so coolant is supplied externally.
Head construction: pocket, insert, clamp, and screw
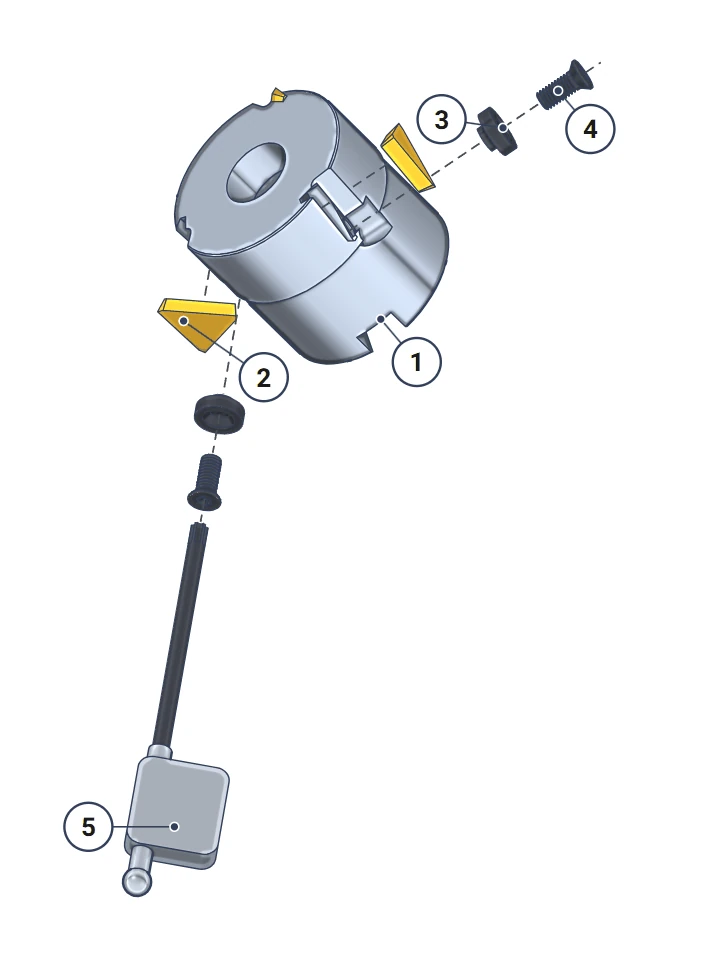
Head components and mounting on a milling arbor
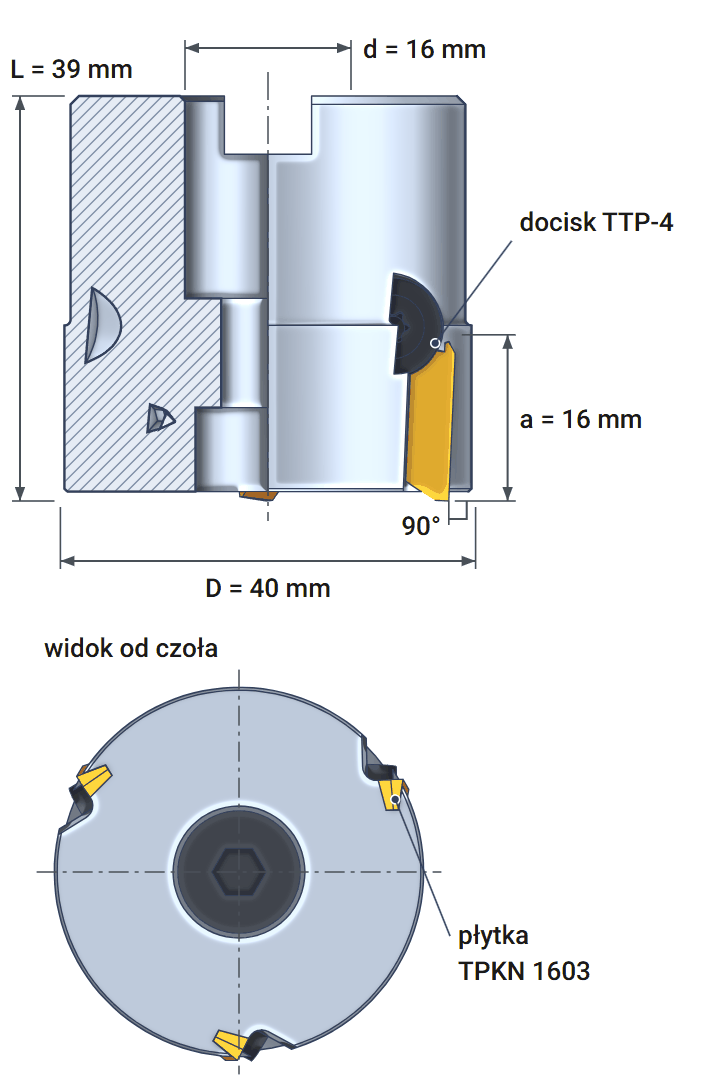
The body has 3 pockets around its circumference. In each pocket, the TPKN 1603 insert rests against two walls. A TTP-4 clamp presses down on its rake face from above, and an M4x10 screw with a Torx T15 recess pulls the clamp down. The insert has no hole, so its cutting edge is continuous along its entire length. The drawing shows two pockets disassembled in removal order: screw, clamp, insert.
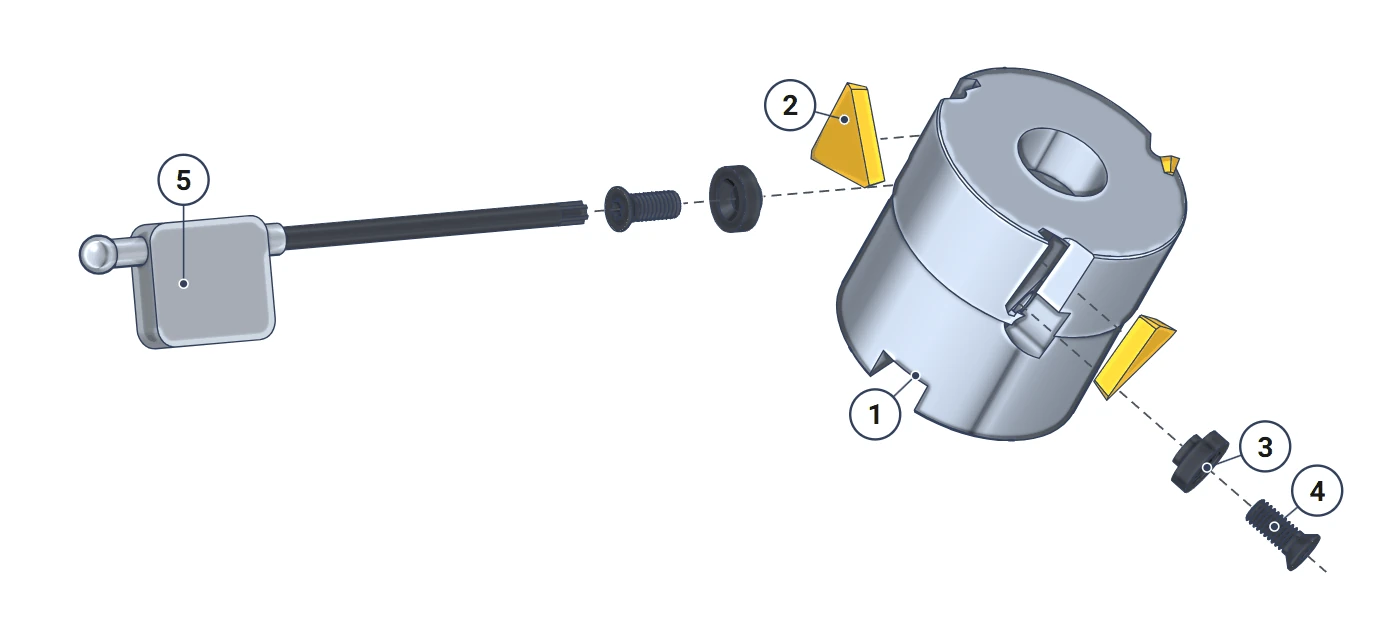
| No. | Part | Quantity | Designation | Wrench |
|---|---|---|---|---|
| 1 | Milling head | 1 | 220.17 D40 Z3 | – |
| 2 | Insert | 3 | TPKN 1603, e.g., TPKN 1603 PDSR | – |
| 3 | Insert clamp | 3 | TTP-4 | – |
| 4 | Clamp screw | 3 | M4x10 | Torx T15 |
| 5 | Torx key | 1 | T15 | – |
Mounting the head on a 16 mm arbor
1Clean the arbor pilot, arbor face, and head bore
2Slide the head on so that the drive keys engage the slot
3Thread the M8 screw into the arbor pilot
✓Head ready for use
A face mill arbor with a 16 mm pilot and 8 mm drive keys is suitable, e.g., 7369 40-16-60 with an SK40 shank to DIN 69871-A or a BT40 arbor to MAS 403-BT. The drive keys engage the transverse slot in the head and transmit torque. The M8 screw only clamps the head against the arbor face. The Smoxh TK90 AP10 D40 head has the same 16 mm bore, so both can use the same arbor.
TPKN 1603 inserts – material selection and replacement
Triangular inserts without a hole, three cutting edges
The head accepts TPKN 1603 inserts to ISO 1832. T denotes an equilateral triangle, and P denotes a 11° clearance angle, indicating a positive insert. K is the tolerance class for inserts with ground lands; N denotes an insert without a hole or chip breaker. The number 16 indicates the edge length in millimeters, and 03 indicates a thickness of 3.18 mm.
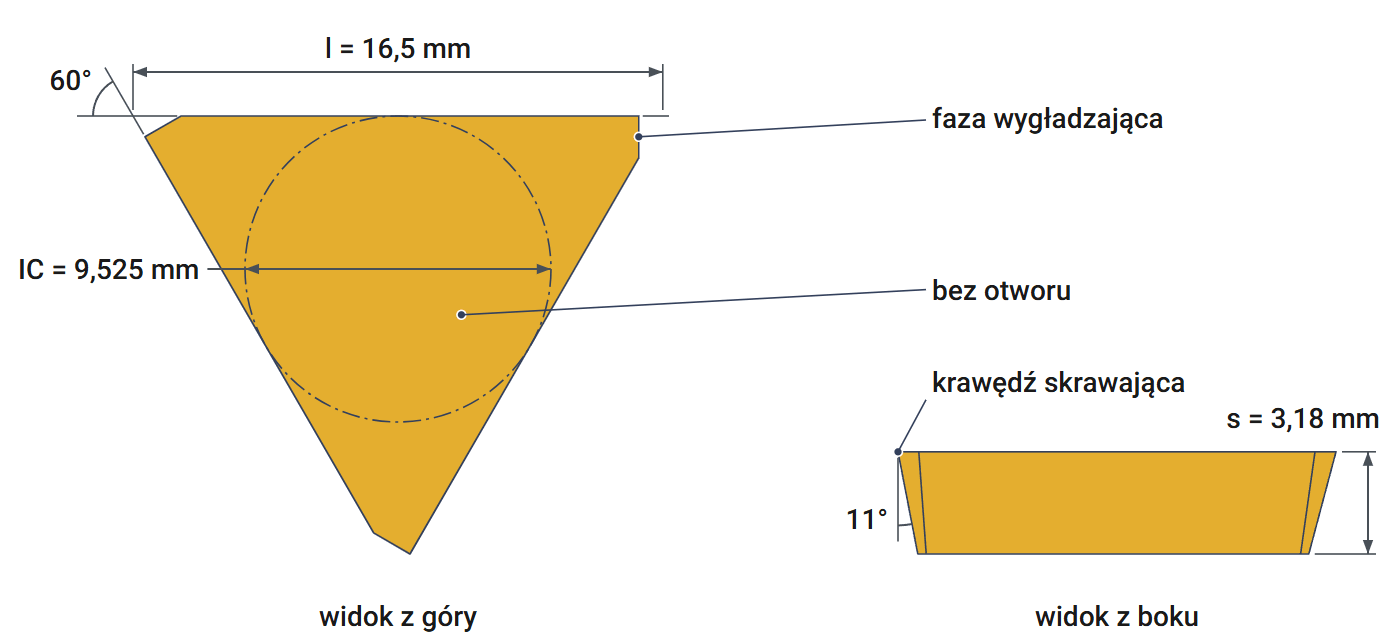
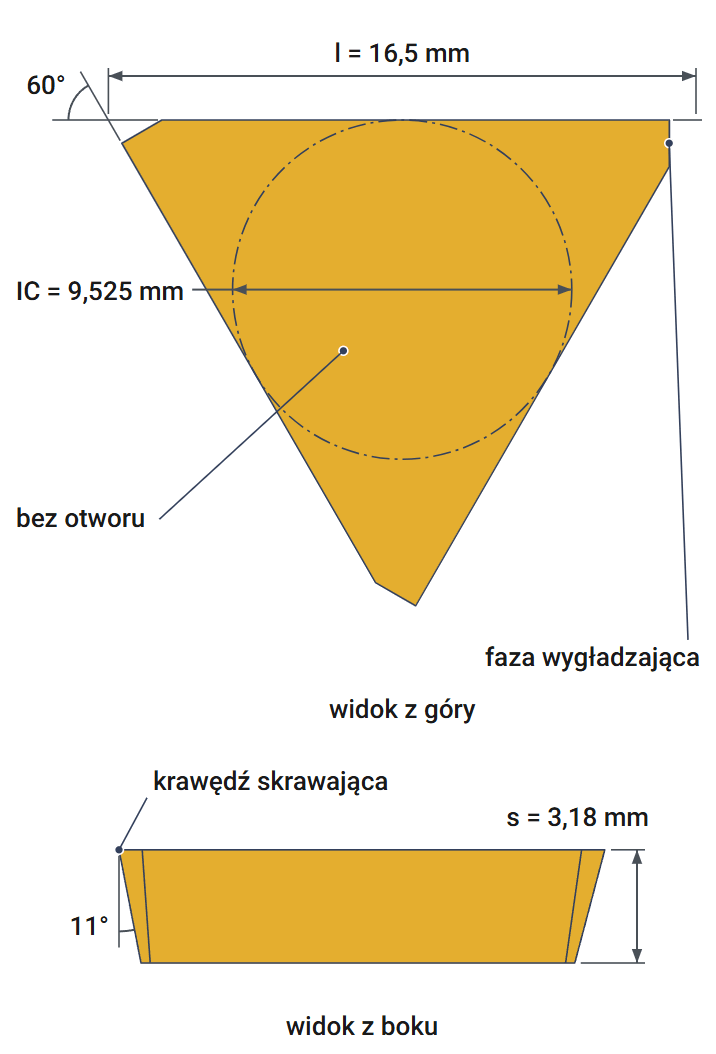
The drawing shows top and side views of the insert. The edge is 16.5 mm long, the inscribed circle is 9.525 mm in diameter, and the thickness is 3.18 mm. The insert has a short wiper land at each corner. In the head, this land lies parallel to the machined surface and finishes the floor. The long edge runs along the axis and produces the shoulder wall.
In the PDSR designation, P indicates a 90° entering angle, D a 15° wiper facet clearance angle, S a chamfered and rounded edge, and R a right-hand insert. The head rotates clockwise, so it requires right-hand inserts with the letter R at the end of the designation.
| Insert | Workpiece material | Notes |
|---|---|---|
| TPKN 1603 PDSR MTC Horn | steel, stainless steel | MTC grade |
Horn is a Korean insert brand available in our store. Any ISO-compliant TPKN 1603 insert fits this head. You can therefore switch workpiece materials by changing only the insert, without replacing the head.
Replacing and indexing the insert
1Loosen the clamp screw with a Torx T15 wrench
2Slide out the insert and remove chips from the pocket and clamp
3Rotate the insert 120° to a new edge
4Press the insert against the pocket walls and tighten the screw
✓New edge in operation
The insert has three cutting edges, one at each corner. A chip under the insert raises it in the pocket and causes runout, so clean the pocket every time you change an insert. Index or replace all 3 inserts together so they cut at the same height.
Face milling and 90° shoulder milling – head operation
What a milling head for TPKN 1603 inserts does
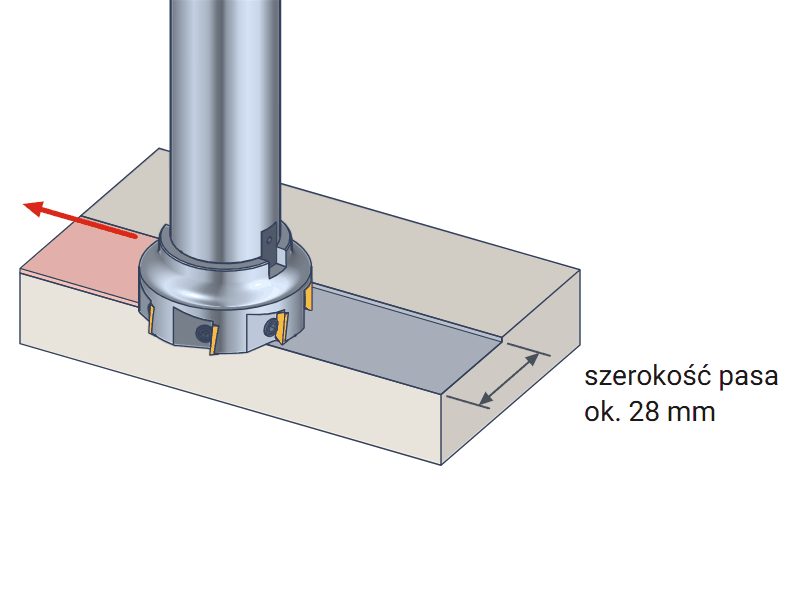
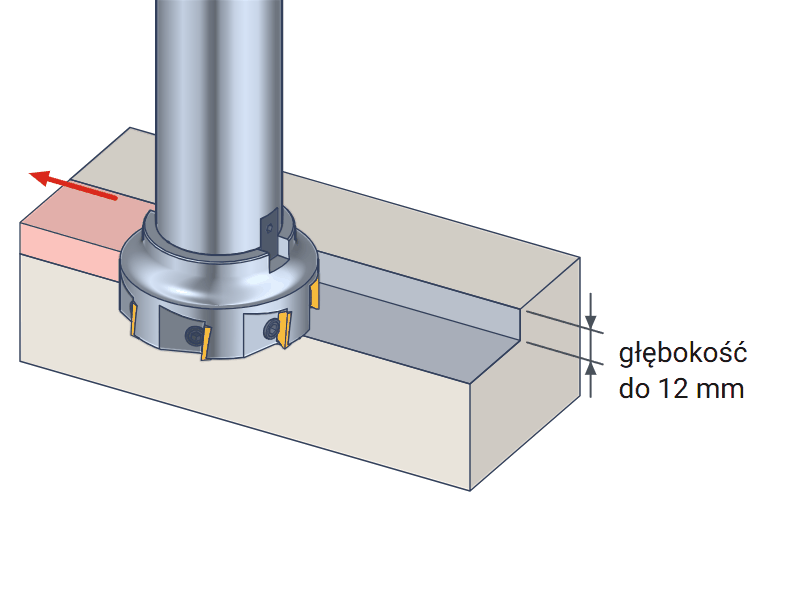
The TPKN 1603 insert is positioned in the milling head with its long edge along the axis. This edge produces a wall perpendicular to the floor. Only the short chamfer at the insert corner cuts on the face. The milling head is therefore used for two operations: face milling and 90° shoulder milling. The drawings show the milling head movement and the material removed.
Face milling
The milling head passes over the workpiece at a shallow depth of cut. The chamfer at the insert corner smooths the surface. One pass removes a strip up to approximately 28 mm wide, or 70 % of the diameter. This is how the milling head face mills end faces, ledges, and castings.
90° shoulder and contour
The long insert edge is parallel to the milling head axis. This produces a wall perpendicular to the floor. A shoulder height of up to 12 mm can be machined in one pass. Mill taller shoulders in several passes.
▲
The milling head cannot plunge into the material
The TPKN 1603 insert cuts on the face only with the chamfer at its corner. Do not enter solid material axially, by ramping, or along a helical path with this milling head – the body will contact the workpiece and overload the inserts. Start each pass from the side of the workpiece.
Cutting data – starting values for 3 inserts
Cutting speed, feed per tooth, spindle speed, and feed rate for a 40 mm milling head
The table provides conservative starting values for face and shoulder milling with TPKN 1603 inserts. Spindle speed and feed rate are calculated for a diameter of 40 mm and 3 inserts. Start with these values and increase them while monitoring the chips and spindle operation.
| Workpiece material | Insert | Cutting speed vc [m/min] | Feed per tooth fz [mm] | Spindle speed [rpm] | Feed rate [mm/min] | Max. depth of cut ap [mm] |
|---|---|---|---|---|---|---|
| P Structural and alloy steel | MTC | 150 (130–200) | 0.10 (0.10–0.20) | 1190 | 360 | 4 |
| M Stainless steel | MTC | 90 (70–130) | 0.08 (0.06–0.15) | 720 | 170 | 2 |
Spindle speed and feed rate calculation – steel, 150 m/min
Spindle speed = 1000 × cutting speed 150 m/min ÷ (3.14 × milling head diameter 40 mm) ≈ 1190 rpm. Feed rate = feed per tooth 0.10 mm × 3 inserts × 1190 rpm ≈ 360 mm/min. Enter these two values in the machine program. In stainless steel, at 90 m/min, the spindle speed drops to approximately 720 rpm.
Ø40 mm milling head Varel 220.17 face mills flat surfaces and mills 90° shoulders in steel and stainless steel. It uses three TPKN 1603 inserts secured by clamps. It mounts on a face mill arbor with a 16 mm pilot and uses external coolant. The maximum depth of cut is 12 mm.
Questions about the 220.17 D40 head
Arbor, inserts, clamping, depth
A face mill arbor with a 16 mm pilot and two 8 mm drive keys, e.g., SK40 to DIN 69871-A (7369 40-16-60) or BT40 to MAS 403-BT. The drive keys engage the transverse slot in the head and transmit torque. An M8 screw threaded into the arbor pilot clamps the head in place.
Right-hand ISO TPKN 1603 inserts, e.g., TPKN 1603 PDSR. Grade MTC from the Korean brand Horn is suitable for steel and stainless steel. Each insert is secured by a TTP-4 clamp with an M4x10 screw.
The TPKN 1603 insert is triangular, has no hole, and has three cutting edges. A clamp holds it in the pocket, leaving the entire edge continuous. The APKT insert has a hole for a Torx screw and two edges.
A shoulder height of up to 12 mm can be machined in one pass. Start with a depth of cut of up to 4 mm in steel and up to 2 mm in stainless steel. When face milling a wide surface, remove a strip up to approximately 28 mm wide.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.