 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
GRADE00 per DIN 875
PERPENDICULARITY0.004 mm
ARMS150 × 100 mm
EDGE70°, lapped
Knife-edge square 150x100 – DIN 875 workshop square
Technical data, grade 00
| Technical data | |
|---|---|
| Standard | DIN 875, form C |
| Accuracy grade | 00 (DIN 875/00) |
| Long arm H | 150 mm |
| Short arm L | 100 mm |
| Arm cross section a × b | 25 × 7.7 mm |
| Perpendicularity tolerance | 0.004 mm |
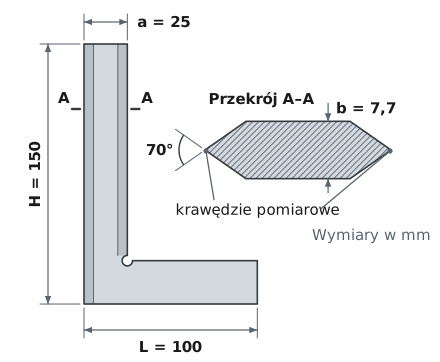
Knife-edge square 150x100 is a right-angle reference of grade 00 per DIN 875 – the most accurate grade in this standard. The long arm has edges beveled at 70° and lapped. It contacts the workpiece along a line rather than across a plane, so a gap as small as approximately 2 µm can be seen against the light. Perpendicularity deviation over a length of 150 mm does not exceed 0.004 mm.
The short 100 mm arm has flat measuring faces and serves as the measurement reference. The 150 × 100 mm size pair comes from the DIN 875 table, and the 150 mm arm covers a workpiece wall up to this height in a single placement. The square is hardened – DIN 875 permits the knife-edge form only in a hardened version.
Square with a measuring edge in practice
Four tasks, one right-angle reference
TASK 01
Checking perpendicularity against the light
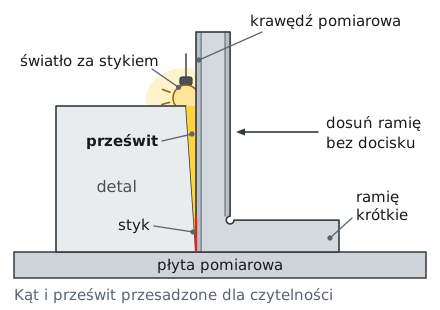
Place the short arm on a surface plate and move the edge of the 150 mm arm against the workpiece face without applying pressure. Position a lamp behind the contact and view the contact line from the front.
✓ Result: the edge contacts the face along a line, so with good lighting a gap as small as approximately 2 µm can be seen. A wedge of light at the top or bottom shows the direction in which the face deviates from 90°.
TASK 02
Flatness and straightness against the light
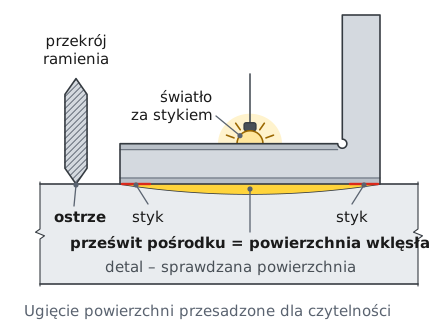
Place the edge of the long arm against the surface being checked, using it as a straight edge. Light behind the contact will reveal any irregularity over the 150 mm length.
✓ Result: a light gap in the middle indicates a concave surface, while gaps at the ends indicate a convex surface. The straightness of the edge itself is within 0.003 mm.
TASK 03
Measuring edge beveled at 70°
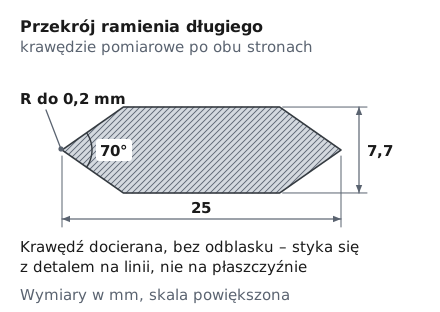
The long arm, with a cross section of 25 × 7.7 mm, has an edge beveled at 70° on both sides. The edge radius does not exceed 0.2 mm, and its surfaces are lapped and nonreflective.
✓ Result: contact with the workpiece along a line rather than across a plane. Metrology textbooks identify this type of square as better for assessing light gaps than a square with a flat surface.
TASK 04
Workpiece corner and shoulder
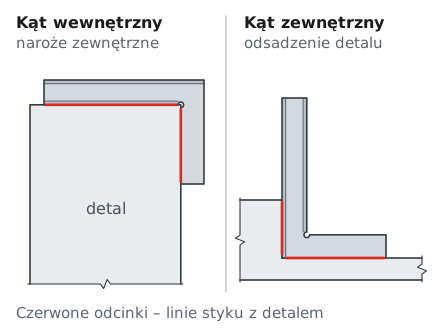
Place the internal angle around the external corner of the workpiece. Use the external angle to check a shoulder: the short arm rests on the bottom, and the edge of the long arm contacts the face.
✓ Result: measuring edges are provided on both sides of the long arm, so the square measures both angles. The corner relief prevents the workpiece edge from bearing against the square.
Grade 00 precision square – what 0.004 mm means
Tolerance zone, calculation, and grade selection
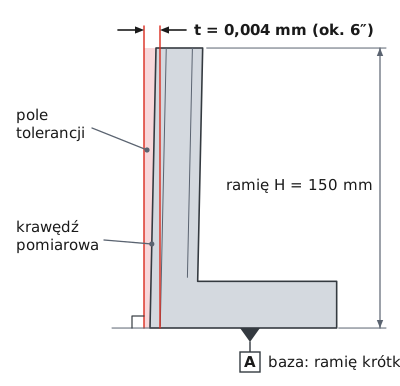
Perpendicularity tolerance is a zone, not a "plus or minus" deviation. Its width for grade 00 is given by the DIN 875 formula.
t = 2 + 150 / 100 = 3.5 µm, rounded according to the standard to 4 µm = 0.004 mm
t – perpendicularity tolerance for grade 00 according to DIN 875: 2 µm plus one hundredth of the arm length in millimeters (1 µm = 0.001 mm). In angular terms, this is approximately 6″ (″ – arcsecond, 60″ = 1 arcminute). At a height of 150 mm, the edge may deviate from true vertical by no more than 0.004 mm – approximately 9 times less than in grade 2 (0.035 mm).
Perpendicularity tolerance of the 150x100 square per DIN 875
| Arm length | Grade 00 | Grade 0 | Grade 1 | Grade 2 |
|---|---|---|---|---|
| 50 mm | 0.003 mm | – | – | – |
| 75 mm | 0.003 mm | 0.007 mm | 0.014 mm | 0.028 mm |
| 100 mm | 0.003 mm | 0.007 mm | 0.015 mm | 0.030 mm |
| 150 mm | 0.004 mm This product | 0.008 mm | 0.018 mm | 0.035 mm |
| 200 mm | 0.004 mm | 0.009 mm | 0.020 mm | 0.040 mm |
| 250 mm | 0.005 mm | 0.010 mm | 0.023 mm | 0.045 mm |
| 300 mm | 0.005 mm | 0.011 mm | 0.025 mm | 0.050 mm |
| 500 mm | 0.007 mm | 0.015 mm | 0.035 mm | 0.070 mm |
| 750 mm | 0.010 mm | 0.020 mm | 0.048 mm | 0.095 mm |
| 1000 mm | 0.012 mm | 0.025 mm | 0.060 mm | 0.120 mm |
Note: perpendicularity tolerance is the zone width referenced to the short arm, not a "±" deviation. Values apply at 20 °C. Grade 00 applies only to knife-edge squares; the standard specifies the 50 mm length only for these squares.
Arm flatness and straightness tolerance per DIN 875
| Arm length | Grade 00 | Grade 0 | Grade 1 | Grade 2 |
|---|---|---|---|---|
| 50 mm | 0.002 mm | 0.003 mm | 0.005 mm | 0.010 mm |
| 70 mm | 0.002 mm | 0.003 mm | 0.005 mm | 0.011 mm |
| 75 mm | 0.002 mm | 0.003 mm | 0.006 mm | 0.011 mm |
| 100 mm | 0.002 mm arm L | 0.003 mm | 0.006 mm | 0.012 mm |
| 130 mm | 0.003 mm | 0.003 mm | 0.007 mm | 0.013 mm |
| 150 mm | 0.003 mm arm H | 0.004 mm | 0.007 mm | 0.014 mm |
| 165 mm | 0.003 mm | 0.004 mm | 0.007 mm | 0.015 mm |
| 200 mm | 0.003 mm | 0.004 mm | 0.008 mm | 0.016 mm |
| 250 mm | 0.003 mm | 0.005 mm | 0.009 mm | 0.018 mm |
| 300 mm | 0.003 mm | 0.005 mm | 0.010 mm | 0.020 mm |
| 500 mm | 0.004 mm | 0.007 mm | 0.014 mm | 0.028 mm |
| 750 mm | 0.005 mm | 0.010 mm | 0.019 mm | 0.038 mm |
| 1000 mm | 0.006 mm | 0.012 mm | 0.024 mm | 0.048 mm |
Note: flatness and straightness apply to each arm separately – the green rows represent arm H and arm L of this square. For the measuring edge, the values apply at inclinations of up to 15° from its plane of symmetry. Values apply at 20 °C.
The workpiece tolerance should be at least 4 times, and preferably 10 times, the instrument tolerance. For 0.004 mm, this gives 0.016 mm (1:4) and 0.04 mm (1:10). The knife-edge square 150x100 can therefore reliably assess perpendicularity with a tolerance of 0.04 mm or greater, or 0.016 mm or greater under the 1:4 rule.
How to check perpendicularity with a knife-edge square
The light gap method step by step
Inspection with a workshop square in 4 steps
1Clean
the square and workpiece, remove burrs from the edges
2Place
the short arm on a surface plate or on the workpiece datum surface
3Move
the edge of the long arm against the face without applying pressure
✓Assess
the gap against the light; measure any visible gap with gauge blocks
The short arm is the measurement datum.
▲
Method limitations
The absence of a light gap does not prove that the workpiece is within its tolerance – only that the deviation is below the method's detection threshold. DIN 875 tolerances apply at 20 °C, and a square warmed in the hand or in sunlight expands. After a drop or impact, check perpendicularity before further use.
The 150x100 knife-edge square combines grade 00, a 70° measuring edge, and a flat 100 mm reference arm. Among DIN 875 workshop squares, only the knife-edge type can meet grade 00 – flat squares and squares with bases are limited to grade 0. This precision square is intended for toolrooms and accurate workpiece inspection. After use, wipe the edges and store it in its case with a thin coat of oil.
Questions about the knife-edge square
Grade, tolerance, calibration
A try square with base (form B according to DIN 875) contacts the workpiece with the flat face of its arm, with a base wider than the arm serving as the reference. A knife-edge square (form C) contacts the workpiece along a narrow edge beveled at 70°. Line contact reveals a smaller light gap, and the standard specifies grade 00 for this form.
No. 0.004 mm is the width of the tolerance zone: the distance between two parallel planes perpendicular to the short arm. The measuring edge of the arm must lie between them. Using “±” suggests a deviation of 0.004 mm in either direction, making the zone twice as wide.
Grade 00 according to DIN 875 is used for highly accurate checks of squareness, flatness, and straightness by the light-gap method, for example in toolrooms. For a 150 mm arm, it permits a deviation of 0.004 mm, so the square can reliably assess the perpendicularity of workpieces with tolerances of 0.04 mm or greater.
Yes, within a small range. DIN 875 specifies edge flatness and straightness tolerances for tilting up to 15° to either side of the edge's plane of symmetry. Within this range, the edge retains the accuracy required by the standard, so slight tilting during positioning does not compromise the measurement.
Squares are not subject to legal metrological control in Poland, so legal verification does not apply. Calibration is voluntary, and its frequency is determined by the user, for example within a quality system. After a drop or impact, check perpendicularity before further use.
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you



Angle tracing gauge 120/200 180 degrees Inox Kinex
€30.75 tax inc.
Last items in stock
Instant Shipping


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.